Rigidity first, accuracy second
Screw drives, heavy guideways and rotary tables for milling, grinding and EDM. The axis has to hold position while the tool pushes back, and stay there after the spindle has warmed up.
Where the axis sits
Six places this industry puts a linear axis. The list is short on purpose — if the machine is not here, the constraint section below still applies.
Vertical machining centres
X, Y and Z axes on box or linear ways, with preloaded screws driving each axis.
Surface and cylindrical grinders
Fine infeed on a short stroke; the screw and the way set the finish, not the control.
EDM and wire EDM
Submersible rotary tables and sealed ways for work that runs under dielectric.
Turn-mill and turret axes
Rotary indexing with a direct-drive table where the turret has to lock and unlock fast.
Laser and plasma gantries
Long travel with a light cutting head; acceleration and straightness trade off against each other.
What the axis has to survive
These three decide the build more often than the load rating does.
Load and vibration
Cutting force arrives as a shock, not a steady push. Carriage size and preload are set for that, not for the catalogue static rating.
Thermal growth
A screw grows with the spindle. Fixed-end and supported-end bearing arrangements decide where that growth goes.
Chips and coolant
Ways and screws need wipers, telescopic covers, or a sealed table when the work runs wet.
Components that fit
Pulled live from the product centre — models this application actually uses.
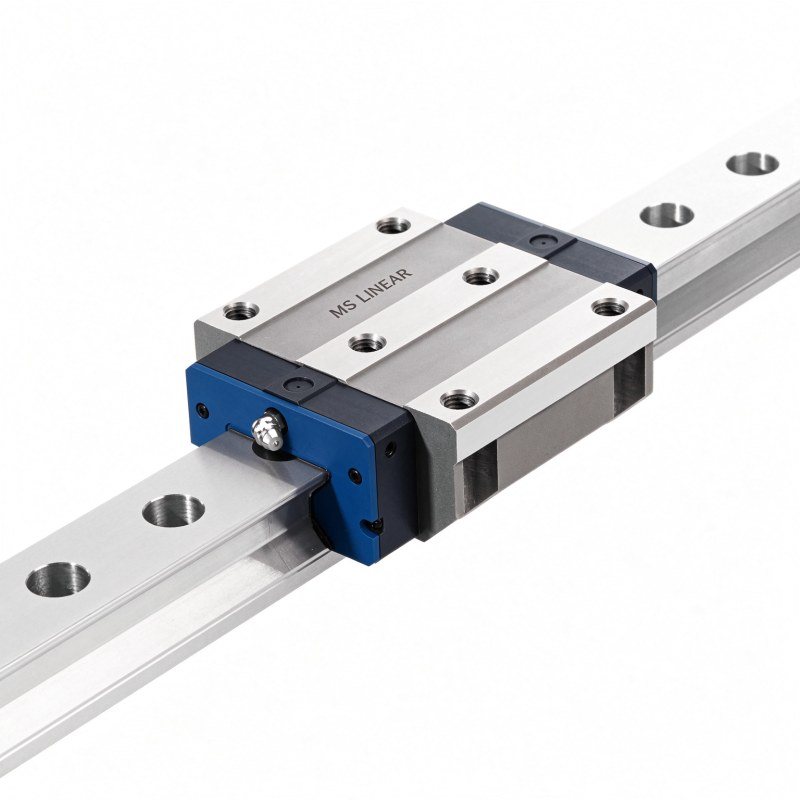
UR Series Ultra-Heavy Load Roller Linear Guideway
Designed specifically for heavy-load and high-precision machining equipment, the UR series…
View model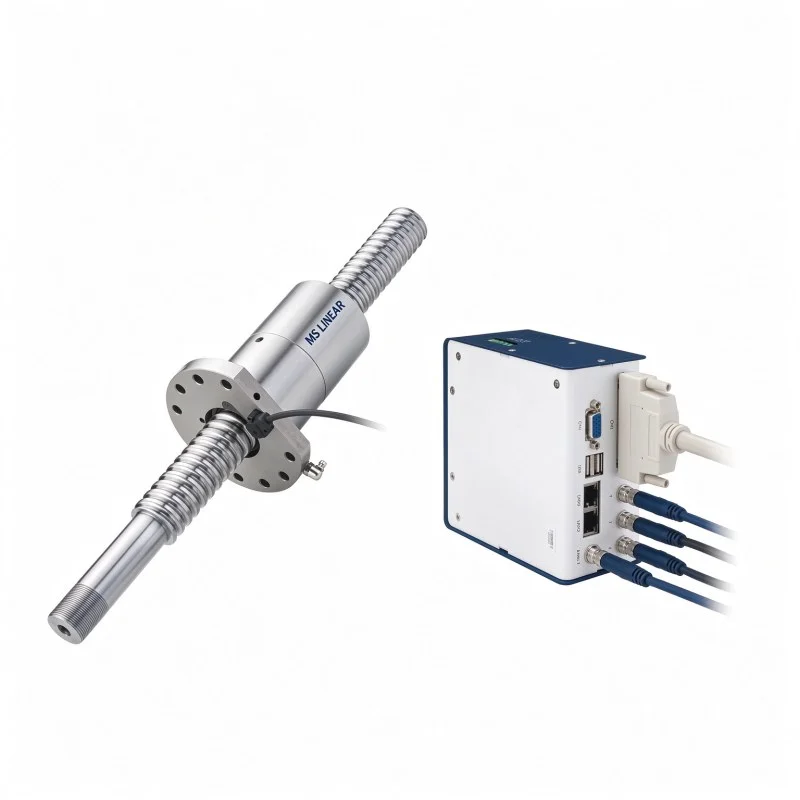
i4.0BS® Intelligent Ball Screw
The ball screw is equipped with sensors and features vibration alerts, temperature…
View model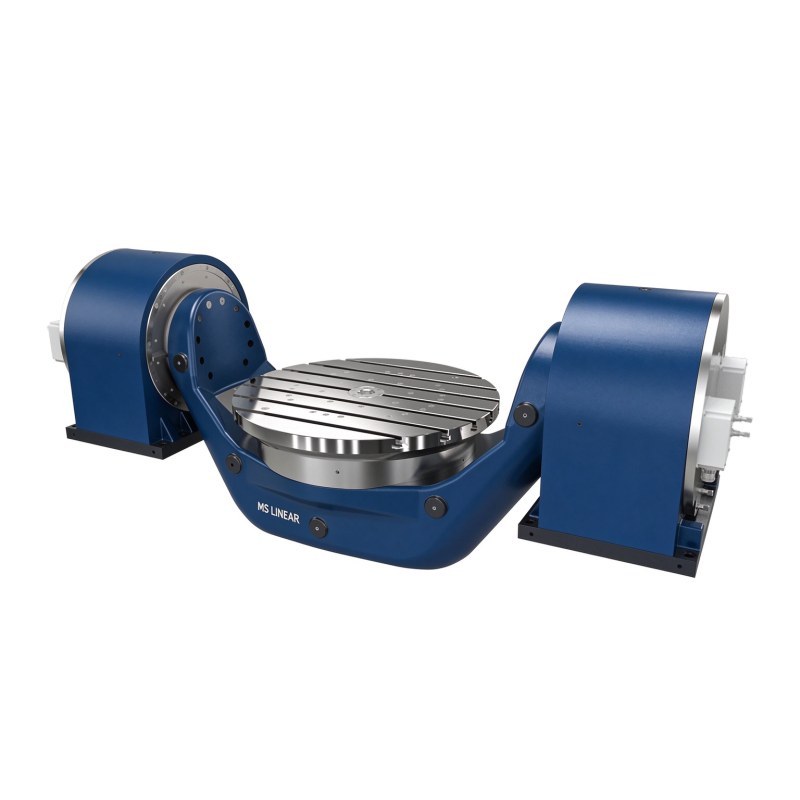
RAB Series Torque Motor Rotary Table
Featuring a direct-drive motor with high acceleration, high torque, high precision and zero…
View model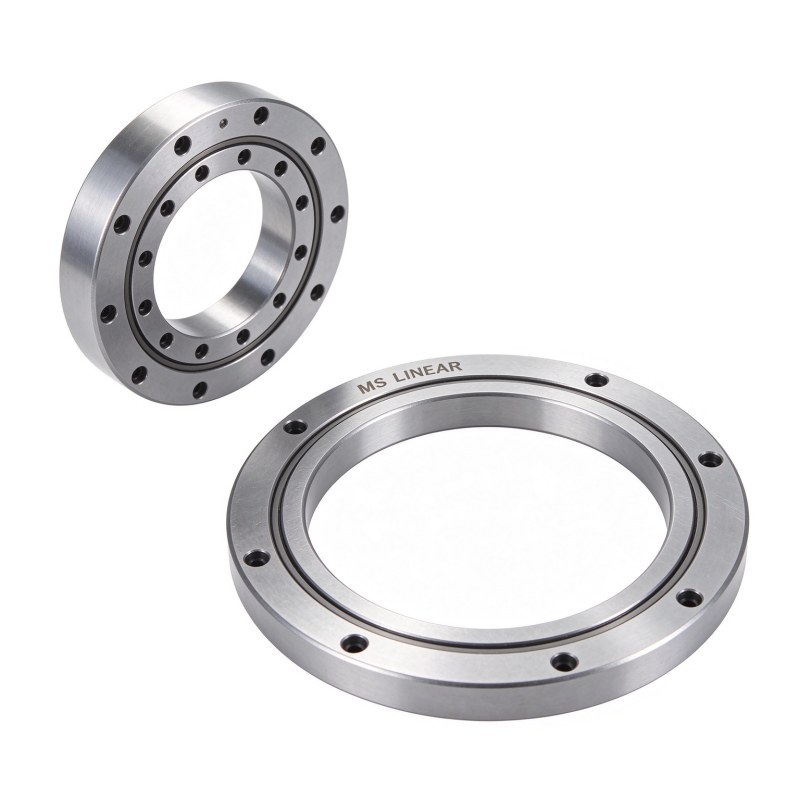
Standard Crossed Roller Bearing
Lightweight construction and space savings increase the machine's effective usable space…
View model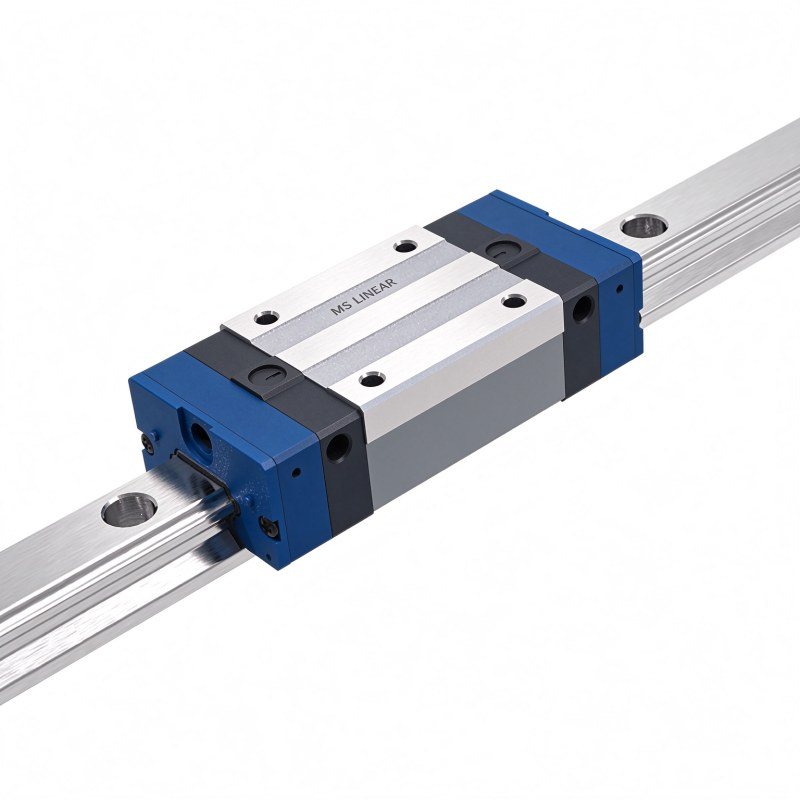
EL Self-Lubricating Linear Guideway
The EL self-lubricating module is specially designed for MG, HG and QH series linear…
View model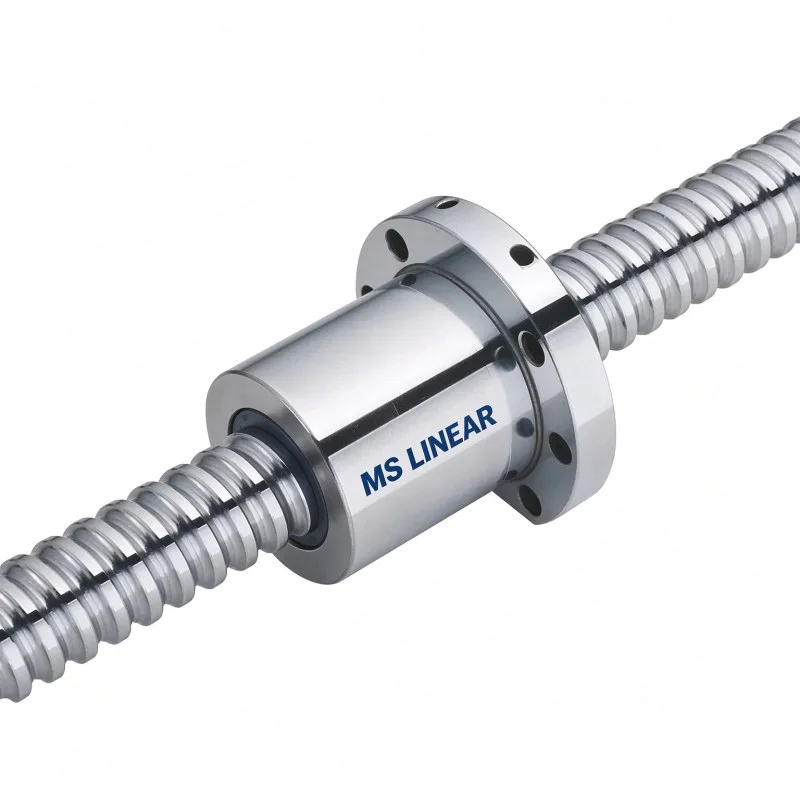
Super S Ball Screw
Low noise, lightweight design, high rotation speed and high acceleration/deceleration.
View modelSelection notes
Three things worth settling before the drawing is frozen.
Preload decides the finish
Light preload for fast moves, medium for cutting. Over-preloading a small screw raises heat without improving the part.
Fix one end of the screw
A fixed-supported arrangement puts thermal growth at the free end. Both ends fixed needs a pre-stretch, and the drawing has to say so.
Wipers are not optional in cast iron
Graphite and chip dust get under a carriage faster than grease gets out. Specify wipers and a cover on anything cutting dry.
Questions that come up
Can you grind a screw to my stroke and end machining?
Yes. Send the drawing with journal diameters, thread length and keyway; screws are cut and end-machined to the drawing rather than trimmed from stock.
Which carriage size for a VMC Z-axis?
It depends on the overhang and the cutting force, not the table weight alone. Send the axis drawing and the machine class and we size the carriage from that.
Do you supply matched rail and carriage sets?
Rails and carriages are packed as matched pairs when ordered together, so preload and clearance are set at the factory.
Are the tables suitable for wet EDM?
The submersible range is built for dielectric immersion, with the seal and cable entry checked with the tank filled.
Buying Machine Tools Motion Components from China
is Your Best Choice!
Factory-direct quality and worldwide shipping — standard parts leave the factory in 3–10 days, custom strokes and leads in 15–20 days (2–3 weeks). Send your drawing or the original part number and get a quotation within 24 hours.
Cookie preferences
Choose which categories this site may use. Necessary cookies cannot be switched off.